
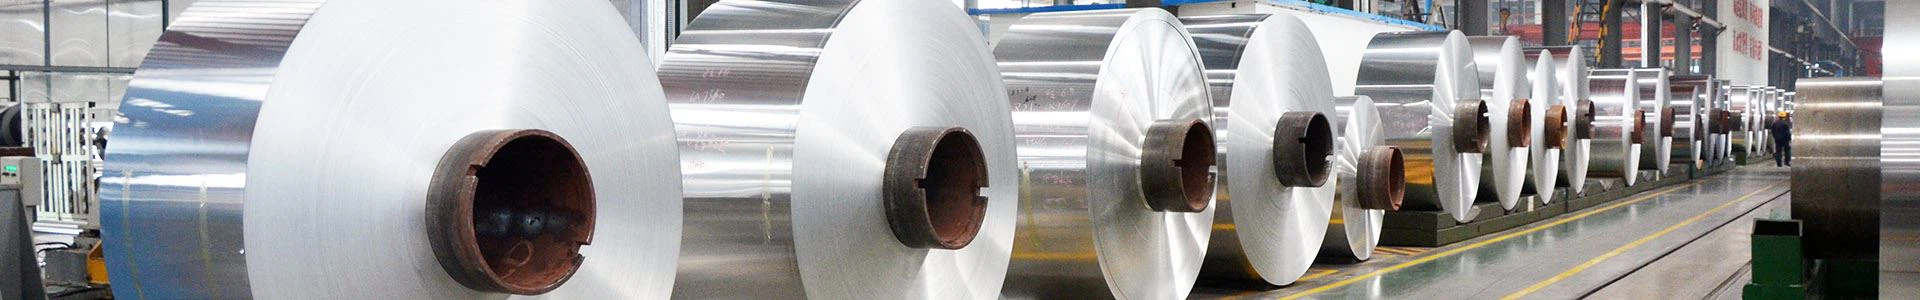
Food‑grade coated aluminum foil is a functional packaging material produced by coating high‑purity aluminum foil substrate with food‑safe resin coatings such as polyester, acrylic resin, epoxy resin and water‑based polyurethane via roll coating or spraying processes. It combines the barrier, light‑shading and heat‑conducting properties of aluminum foil with the corrosion‑resistant, oil‑proof, heat‑resistant, formable and non‑stick advantages of coatings. As an irreplaceable core material in modern food packaging, it is widely used in baking, cooked food, snacks, cold‑chain products, catering, prepared dishes and other fields.
Core Performance Advantages (Meeting Requirements of Modern Food Packaging)
High‑barrier protection: Aluminum foil itself blocks oxygen, moisture, light and odors. Coatings further enhance resistance to acid, alkali and grease, preventing food oxidation, deterioration, moisture absorption and odor mixing to extend shelf life.
Safety compliance: The coatings are food‑contact‑grade with no heavy metals or harmful substances released. Heat‑resistant for microwave or oven heating, they meet domestic and international food‑contact safety standards.
Wide temperature adaptability: Tolerant to cold storage at ‑40 °C and high‑temperature baking, grilling and steaming above 200 °C, suitable for heating needs of prepared and instant foods.
Excellent formability and processability: Coatings improve flexibility and anti‑cracking performance, enabling stamping, heat‑sealing and lamination for high‑speed automated packaging production lines.
Sanitary and antibacterial: The dense and smooth surface resists bacterial growth, water and oil penetration, satisfying hygiene requirements for takeaway and ready‑to‑eat foods.

Main Application Scenarios
Baking and Grilling Packaging
Used for baking mat paper, barbecue foil, tart cups, cake liners and pizza pads. The non‑stick and heat‑resistant coatings allow easy food release, suitable for home baking and standardized commercial kitchen applications.
Prepared and Instant‑Heat Food Packaging
Aluminum foil containers, retort pouches and inner liners for self‑heating hot pot and rice. Coatings resist high‑temperature steaming and corrosion from acidic or alkaline soup, supporting microwave or open‑flame heating. Strong sealing preserves flavor and freshness to fit fast‑paced modern catering consumption.
Snack Food Packaging
Inner packaging for chocolate, candy, cheese, nuts and potato chips. It blocks light, oxygen and moisture to prevent grease oxidation and rancidity, while oil‑proof and non‑stick coatings improve packaging quality and shelf life.
Dairy and Cold‑Chain Fresh‑Food Packaging
Lids for yogurt cups, cheese packaging and vacuum inner wrapping for fresh meat and seafood. Light‑blocking properties prevent vitamin loss, and low‑temperature resistance ensures fresh‑food protection throughout cold‑chain logistics.
Takeaway and Disposable Catering Packaging
Aluminum foil takeaway boxes and sauce cup lids. Oil‑proof, leak‑proof and heat‑resistant, they support secondary microwave heating. More eco‑friendly and free of plasticizer risks than plastic alternatives, ideal for high‑end takeaway and group catering markets.
Tea, Dry Goods and Health‑Food Packaging
Composite inner aluminum foil prevents tea oxidation and dry‑goods mildew from moisture and light. Coatings enhance printing adhesion for brand logos and food information.
Infant Complementary Food and Special Dietary Packaging
High‑purity aluminum foil with food‑grade coatings delivers superior safety and barrier performance for pureed baby food, nutritional powder and special‑diet products under strict hygiene standards.

Application Trends in the Modern Food Industry
Lightweight and eco‑friendly: Thin high‑toughness coated aluminum foil replaces thick aluminum foil and partial plastic packaging, recyclable and biodegradable in line with green packaging policies.
Multi‑functional upgrading: Heat‑resistant retort, antibacterial, easy‑tear and heat‑sealable coated aluminum foil are rapidly popularized, driven by booming prepared and instant‑heat food markets.
High‑end customization: Matte, colored and printable coated aluminum foil is adopted for premium snacks and gift‑packaged foods to enhance product grade.
Smart packaging compatibility: Anti‑counterfeit and traceability coatings can be added to realize digital management of food packaging.
Conclusion
With comprehensive advantages of safety, high barrier, heat resistance, fresh‑keeping and easy processing, food‑grade coated aluminum foil perfectly adapts to the modern food industry's trends of prefabrication, instant consumption, cold‑chain logistics and convenience. It serves as a key material for packaging upgrading from traditional plastics to eco‑friendly metal flexible packaging, and its application scale will keep expanding in prepared dishes, baking and high‑end snack sectors in the future.